NSIC ISO 9001:2015 & TUV AUSTRIA CERT COMPANY
Agitators & Reactors
Other Equipment
PM INDUSTRIES · OTHER EQUIPMENT
OTHER EQUIPMENT

Agitators & Reactors

Controlled agitation, heat transfer and reactions.

LiquidsSlurries
Application
Wet mixing · Reaction
Capacity / working range
50 – 20,000 L
Engineering
Configured to your process requirements

Agitators & Reactors

Agitators & Reactors Overview

Agitators and Reactors are vital equipment for mixing, chemical reactions, and process intensification in various industries including pharmaceuticals, chemicals, food, and petrochemicals. PM Industries designs and manufactures a wide range of agitators and reactors customized to handle a variety of mixing and reaction needs from simple blending to complex chemical synthesis.

Our reactors and agitators are engineered for robust performance, uniform mixing, precise temperature control, and scalability.

Working Principle

  • Agitators: Mechanical mixing devices that induce fluid motion to ensure uniformity, suspension of solids, heat transfer, or chemical reaction facilitation within a vessel. Agitator types include turbine, paddle, anchor, and propeller designs.
  • Reactors: Vessels designed for controlled chemical reactions with integrated mixing, heating/cooling jackets, and instrumentation for process monitoring.

Key Features

  • Customizable agitator types for various viscosities and process requirements
  • Reactors available in batch, semi-batch, and continuous modes
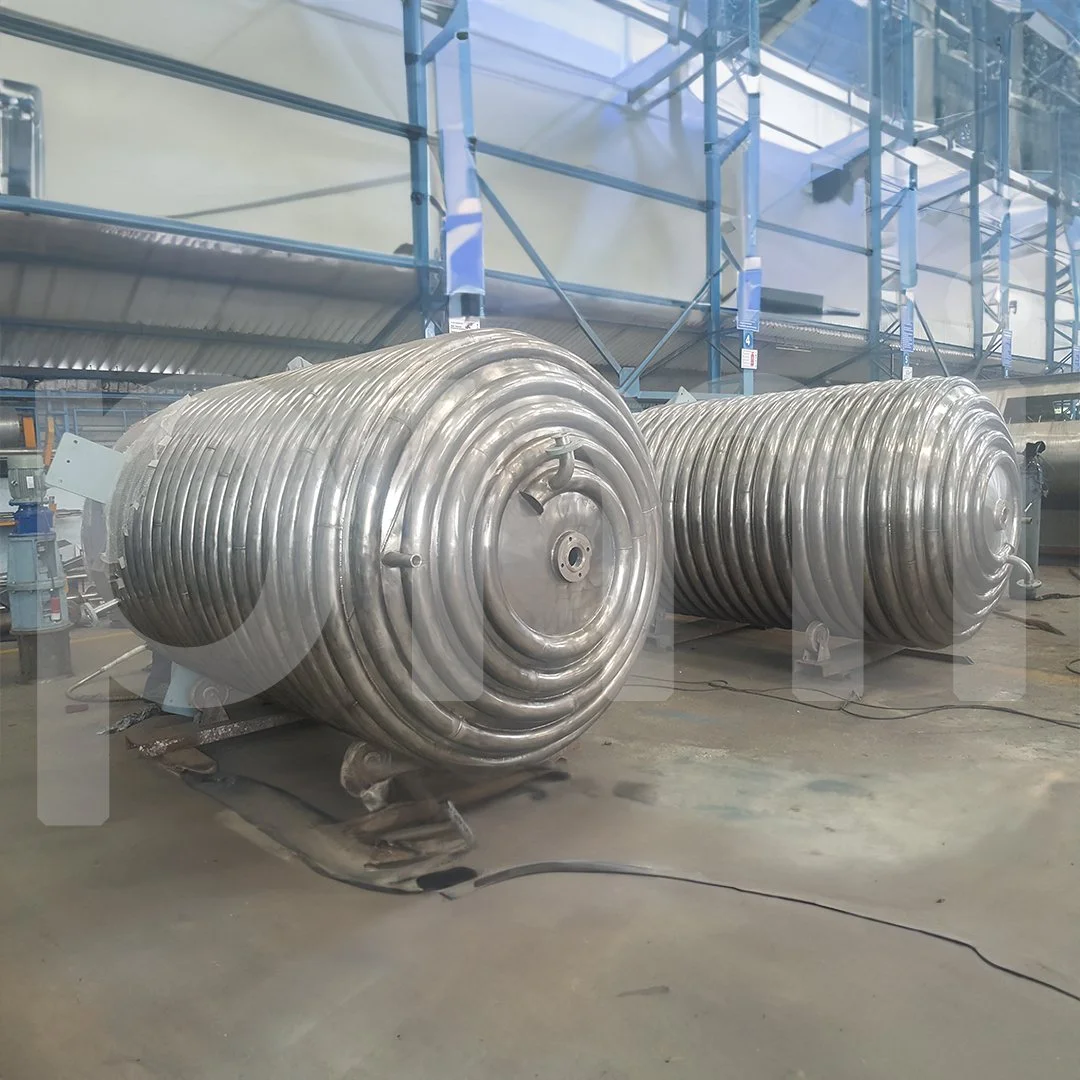
  • Jacketed or coil-equipped reactors for precise thermal management
  • High-quality materials (SS 304, SS 316L, Hastelloy) for chemical resistance
  • Variable speed drives and advanced control systems for optimized mixing
  • CIP (Clean-in-Place) and SIP (Sterilize-in-Place) options
  • Designed to meet ASME, PED, and GMP standards

Applications

  • Pharmaceutical drug synthesis and formulation
  • Chemical process reactions including polymerization and crystallization
  • Food and beverage blending and fermentation
  • Agrochemical synthesis and formulation
  • Biotech fermenters and cell culture reactors

Technical Specifications

ParameterSpecification RangeRemarks
Reactor Volume50 – 20,000 LitersCustom designed per process requirements
Agitator TypesTurbine, Paddle, Anchor, PropellerSelected based on viscosity and mixing needs
Drive Power1 – 100 kWVariable frequency drives for speed control
Vessel MaterialSS 304 / SS 316L / HastelloyDepending on chemical compatibility
Operating PressureAtmospheric to 10 barCustom pressure ratings available
Operating TemperatureAmbient to 250 °CJacketed and coil options for heating/cooling
SealingMechanical seals / Magnetic couplingsFor leak-proof operation
Control SystemsPLC with HMIFor automation and precise process control

Variants Available

  • Batch Reactors – Flexible and widely used for multiple reactions
  • Continuous Reactors – For steady-state operation and high throughput
  • Jacketed Reactors – For controlled temperature processes
  • Agitators for High Viscosity – Anchor and paddle designs for thick fluids
  • Explosion-Proof Designs – For hazardous environments (ATEX certified)

Downloads

Need precision mixing and reaction solutions?

PM Industries And Process Equipments Private Limited provides agitators and reactors designed for your process scale and complexity.

FIND THE RIGHT APPLICATION

Explore where it’s used.

LET’S TALK ABOUT YOUR PROCESS

Your requirement.
Our engineering expertise.

Tell us what you’re making and how you want to improve it. Our team can help you explore the right equipment.

Discuss your project
YOUR EQUIPMENT SHORTLIST

Compare your options.

Ranges depend on configuration. Discuss your material and process with our engineers to confirm suitability.